Specializing in the production of Plastic Pulverizer Machines.

Views: 0 Author: Site Editor Publish Time: 2026-09-29 Origin: Site
When purchasing plastic pulverizer blades, the key question is not whether a supplier simply describes them as “wear-resistant,” but whether their wear resistance can be measured and verified through actual production data.
Blade material, heat treatment, hardness, geometry, machining accuracy, processed material, and operating conditions all affect blade wear and service life. Therefore, no single parameter can accurately represent the overall performance of a blade.
A more reliable evaluation method is to establish a complete testing process:
Initial Blade Condition → Controlled Production Test → Post-Test Blade Condition and Production Data
By comparing the blade condition before and after testing, together with actual material throughput, powder particle size, output, and operating parameters, buyers can evaluate actual blade wear and make more informed technical and cost comparisons between blade suppliers.
Plastic pulverizer blades are exposed to different mechanical and thermal loads depending on the processed material and production conditions.
Abrasive wear is a common form of blade wear. During continuous pulverizing, hard particles in the material repeatedly contact and rub against the blade surface, gradually dulling the cutting edge and removing material from the working surface.
Different plastics create different wear conditions. Pure PE or PP generally presents a different wear environment from PVC containing mineral fillers such as calcium carbonate. Glass-fiber-reinforced plastics may generate higher abrasive loads.
Therefore, blade wear resistance should not be evaluated based on material grade or hardness alone. The actual processed material, filler content, and production conditions must also be considered.
Plastic pulverizer blades experience repeated mechanical impacts and loads during operation. If the blade lacks sufficient toughness, the cutting edge may develop chips, notches, or cracks.
Such damage reduces the effective working surface and may alter the blade geometry, affecting pulverizing efficiency, particle size consistency, and operating stability.
Therefore, blade wear testing should assess not only material loss but also cutting-edge integrity and changes in blade geometry.
During pulverizing, blades are continuously exposed to friction and thermal loads. Unstable feeding, excessive grinding loads, or unsuitable operating parameters may increase blade temperature and mechanical stress, accelerating wear.
In recycled plastics, hard foreign materials such as metal particles and stones may also cause localized impact damage and cutting-edge chipping.
Therefore, blade service life depends not only on the blade itself but also on feeding stability, operating parameters, cooling conditions, and material cleanliness.
Plastic pulverizer blade wear resistance is determined by a combination of material, manufacturing process, blade design, and operating conditions.
Factor | Main Role |
|---|---|
Steel Grade | Provides basic mechanical properties and wear resistance |
Heat Treatment | Affects hardness, toughness, and dimensional stability |
Hardness | Improves resistance to wear and deformation |
Toughness | Reduces the risk of edge chipping and cracking |
Blade Geometry | Affects pulverizing efficiency and grinding gap |
Machining Accuracy | Helps maintain installation and operating consistency |
Processed Material | Determines the actual wear environment |
Operating Conditions | Affect load, temperature, output, and service life |
Therefore, blade wear resistance should not be evaluated based only on the steel grade or hardness. Blade manufacturing quality must be considered together with the actual production conditions.

D2 and DC53 are both tool steels used in wear-resistant tooling applications. However, for plastic pulverizer blades, comparing steel grades alone cannot fully determine the final blade performance.
A more meaningful comparison should consider heat treatment, hardness, toughness, blade geometry, machining quality, processed material, and operating conditions.
Factor | D2 | DC53 |
|---|---|---|
Tool Steel Application | Wear-resistant tooling | Wear-resistant tooling |
Hardness | Depends on heat treatment | Depends on heat treatment |
Toughness | Depends on heat treatment and blade design | Depends on heat treatment and blade design |
Wear Performance | Depends on actual operating conditions | Depends on actual operating conditions |
Final Blade Performance | Material + heat treatment + geometry | Material + heat treatment + geometry |
Therefore, a meaningful comparison between D2 and DC53 blades should consider the actual processed material, heat treatment condition, hardness, blade geometry, and production results, rather than comparing steel grades alone.

Hardness is an important indicator of plastic pulverizer blade material performance, but higher hardness does not necessarily mean longer service life. An HRC value reflects a material’s resistance to deformation and surface wear, but it cannot directly indicate how many hours a blade can operate or how many tons of plastic it can process.
Even when two sets of blades have similar hardness values, their actual service life can still vary due to differences in toughness, heat treatment, cutting-edge geometry, machining accuracy, processed material, and operating load.
These three concepts can therefore be distinguished as follows:
Hardness → Material Property
Wear Rate → Wear Behavior
Service Life → Operating Time or Material Throughput Before the Defined Replacement Criteria Are Reached
For blade procurement, the most useful reference is not a single HRC value, but actual wear data and production results.
Hardness testing is mainly used to verify the material and heat treatment condition of the blade and is an important part of blade quality control.
Test records can include the steel grade, heat treatment condition, measurement location, and actual HRC value, providing a basis for quality traceability and comparison between different production batches.
However, hardness only reflects material properties and cannot be directly converted into blade service life. Therefore, hardness testing should be used as a basic quality indicator, together with actual wear and production data, to evaluate blade service life.

Measuring key blade dimensions before and after testing can directly show dimensional changes and material loss, making it an important method for evaluating actual blade wear.
To ensure data comparability, the measurement locations, tools, and methods should remain consistent before and after testing, and the dimensional differences should be recorded.
These measurements can then be used to calculate blade wear and wear rate, providing a basis for comparing the performance of different blades.
Cutting-edge wear can be evaluated by measuring:
Cutting-edge retreat
Changes in edge profile
Wear on the working surface
Other defined changes in critical blade dimensions
The key is not to rely on one specific measurement method, but to maintain consistent measurement locations, methods, and evaluation criteria before and after testing. This makes the wear results more reliable and comparable.
A meaningful blade wear test should control the variables that may affect the results. The goal is to keep the test conditions as consistent as possible so that differences in blade wear can be evaluated more reliably.
Before starting the production test, record:
Blade material
Hardness
Key dimensions
Cutting-edge condition
Blade geometry
Installation condition
These records provide the baseline for comparison after the test.
When comparing two blade solutions, use the same type and similar condition of processed material whenever possible to minimize the influence of material differences.
For example, a test using pure PE cannot be directly compared with a test using glass-fiber-reinforced plastic because the two materials create different wear environments and mechanical loads.
The following test parameters should be recorded:
Test Parameter | Recommended Record |
|---|---|
Pulverizer Model | Model and disc diameter |
Blade Material | Steel grade and specifications |
Processed Material | Plastic type and formulation |
Feed Size | Initial material size |
Target Powder Size | Mesh or micron range |
Feed Rate | kg/h |
Motor Power | Installed motor power |
Grinding Gap | Initial working gap |
Cooling Method | Air, water, or combined cooling |
Operating Time | Actual test duration |
Throughput | Total amount of material processed |
The more consistent the test conditions are, the more comparable the blade wear data will be, making it easier to evaluate the actual performance of different blade solutions.

Blade wear should not be evaluated only by changes in the blade itself. Production data should also be recorded to determine how blade wear affects actual operating performance.
Key parameters to record during the test include:
Output: kg/h and total material throughput
Material temperature: to monitor friction and temperature rise
Motor current or load: to identify changes in operating load
Powder particle size and particle size distribution: to evaluate powder consistency
Vibration and abnormal conditions: to identify changes in machine operation
Powder collection: to check whether discharge and collection remain stable
Comparing these production data with measured blade wear can help determine whether blade wear has affected output, powder quality, or equipment operating stability.
Operating hours alone are not enough to fully evaluate blade wear. Two machines may operate for the same number of hours while processing very different amounts of material.
In a controlled comparison test, actual material throughput can therefore be used as an important reference.
A simple calculation is:
Wear Rate = Measured Blade Material Loss ÷ Actual Material Throughput
Depending on the measurement method, wear rate can be expressed as dimensional loss per ton of material, mass loss per ton, or another clearly defined measurement.
For example, if a specified blade dimension decreases by 0.20 mm after processing 100 tons of material:
Dimensional Wear Rate = 0.20 mm ÷ 100 tons = 0.002 mm/ton
The test results should always be reported together with the measurement method, processed material, and test conditions to ensure that the data can be properly interpreted and compared.
Blade Condition | Impact on Production |
|---|---|
Cutting-edge wear | Reduced pulverizing efficiency |
Changes in blade geometry | Changes in grinding conditions |
Excessive wear | Unstable particle size or reduced output |
Increased friction | Higher material temperature |
Severe blade damage | Abnormal vibration or unstable operation |
The key is to determine when blade wear becomes significant enough to affect production targets.
A blade may still be mechanically capable of operating, but its wear may already be affecting powder quality, output, or temperature control beyond the required production specifications.
Replacement Indicator | Meaning |
|---|---|
Excessive dimensional loss | The specified wear limit has been reached |
Cutting-edge damage | The working geometry has been affected |
Unstable particle size | Powder specifications can no longer be maintained consistently |
Reduced output | Production capacity falls below the required level |
Abnormal temperature | The grinding condition has changed |
Abnormal motor load | Operating resistance has changed |
Increased maintenance frequency | Continued operation is becoming less economical |
The specific replacement criteria should be determined based on the blade design, pulverizer model, processed material, and production requirements.
Different plastics create different working conditions for pulverizer blades. Therefore, blade selection should be based on the actual processed material and production conditions.
Material | Key Wear Considerations |
|---|---|
PE / PP | Feed rate, particle size, and thermal conditions |
PVC | Formulation, filler content, temperature, and material properties |
Color Masterbatch | Formulation, granule characteristics, and contamination control |
Engineering Plastics | Material grade, mechanical properties, and thermal behavior |
Filled Plastics | Mineral fillers, glass fibers, and abrasive materials |
Recycled Plastics | Contaminants, metal particles, and foreign materials |
The same blade specification does not automatically provide the same service life across different plastics.
Therefore, blade selection and wear evaluation should start with the actual material and its production conditions.
Test results from pure PE cannot be directly compared with results from glass-fiber-reinforced plastics because they create different wear and mechanical load conditions.
A higher HRC value does not automatically mean a longer blade service life.
Operating hours alone do not fully reflect the actual workload of a blade. The total amount of material processed should also be considered.
A blade may still be mechanically capable of operating, while its wear has already affected particle size, output, or temperature control.
If the feed rate, grinding gap, cooling method, and processed material are changed simultaneously, it becomes difficult to determine which factor caused the difference in blade wear.
When purchasing plastic pulverizer blades, do not ask only, “How much does one set of blades cost?”
It is also important to ask the manufacturer for measurable technical data that can be used for performance and cost comparisons.
Data | Purpose |
|---|---|
Steel Grade | Confirms the blade material |
Heat Treatment | Shows the final mechanical condition |
Hardness | Verifies the heat treatment result |
Blade Dimensions | Confirms equipment compatibility |
Cutting-Edge Geometry | Affects pulverizing performance |
Test Material | Defines the actual wear environment |
Throughput | Indicates production capacity |
Operating Time | Defines the test duration |
Total Throughput | Reflects the actual working load |
Wear per Ton | Helps compare wear rates |
Powder Quality | Reflects actual production performance |
Replacement Interval | Supports maintenance planning |
This approach shifts blade procurement from a price-only comparison to a measurable comparison of production performance, wear, and operating cost.
Purchasing Criteria | What to Confirm |
|---|---|
Blade Material | Steel grade |
Heat Treatment | Heat treatment process and hardness |
Machining | Dimensions and blade geometry |
Inspection | Hardness and dimensional inspection |
Compatibility | Pulverizer model and grinding disc |
Testing | Testing with the actual processed material |
Replacement | Replacement blade support |
Service | Installation and technical support |
Plastic pulverizer blades do not operate as independent components. Rotating blades, fixed blades or teeth, grinding discs, grinding chambers, rotors, feeding systems, cooling systems, and grinding gap adjustment systems need to work together as an integrated system.
Therefore, dimensional and geometric compatibility is particularly important when replacing pulverizer blades.
The original equipment manufacturer can evaluate replacement blades based on factors such as:
Pulverizer model
Grinding disc diameter
Blade geometry
Operating speed
Grinding gap
Processed material
Cooling configuration
Installation requirements
This is especially important for customers who want to replace worn blades without replacing their existing plastic pulverizer.
Mao Yue independently develops and manufactures core components for plastic pulverizing systems, including grinding discs, rotating blades, fixed blades, tooth plates, and other wear parts.
The manufacturing process combines material selection, heat treatment, CNC machining, precision grinding, dimensional inspection, hardness testing, cutting-edge inspection, and dynamic balancing.
The goal is not simply to manufacture a high-hardness blade, but to ensure that the blade operates reliably as part of the complete plastic pulverizing system.
For different materials and production requirements, factors such as blade material, hardness, geometry, grinding gap, cooling, feeding, and equipment parameters can be considered as an integrated system.
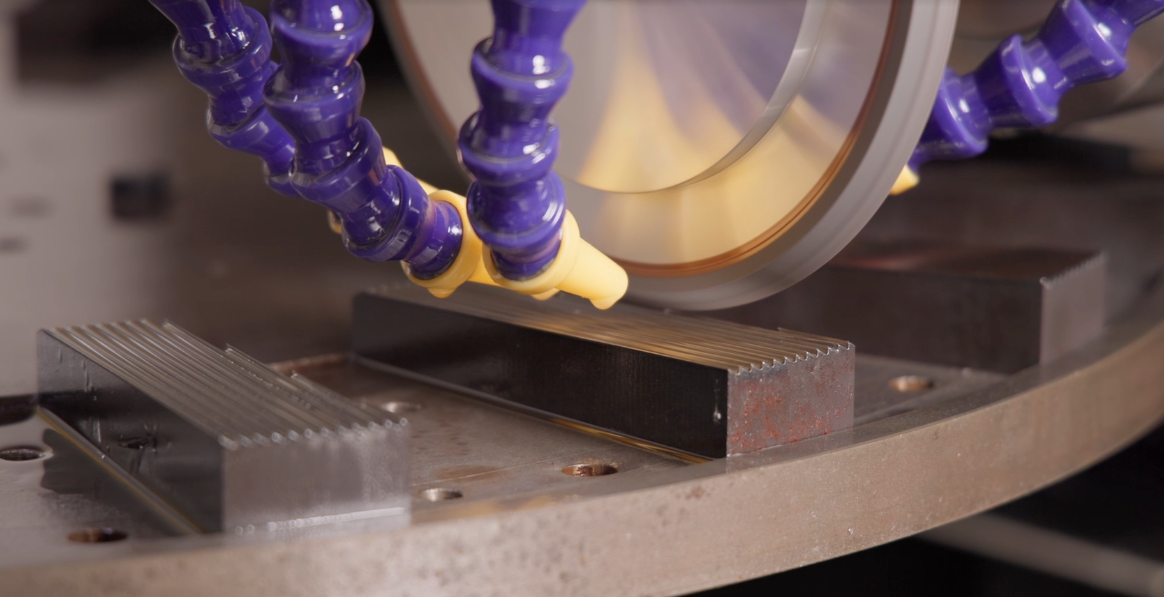
Mao Yue manufactures key wear parts for plastic pulverizers in-house and uses CNC machining to control blade dimensions and geometry.
When blade components and the plastic pulverizer are developed within the same system, blade geometry, grinding gap, rotor speed, and actual material applications can be evaluated together.
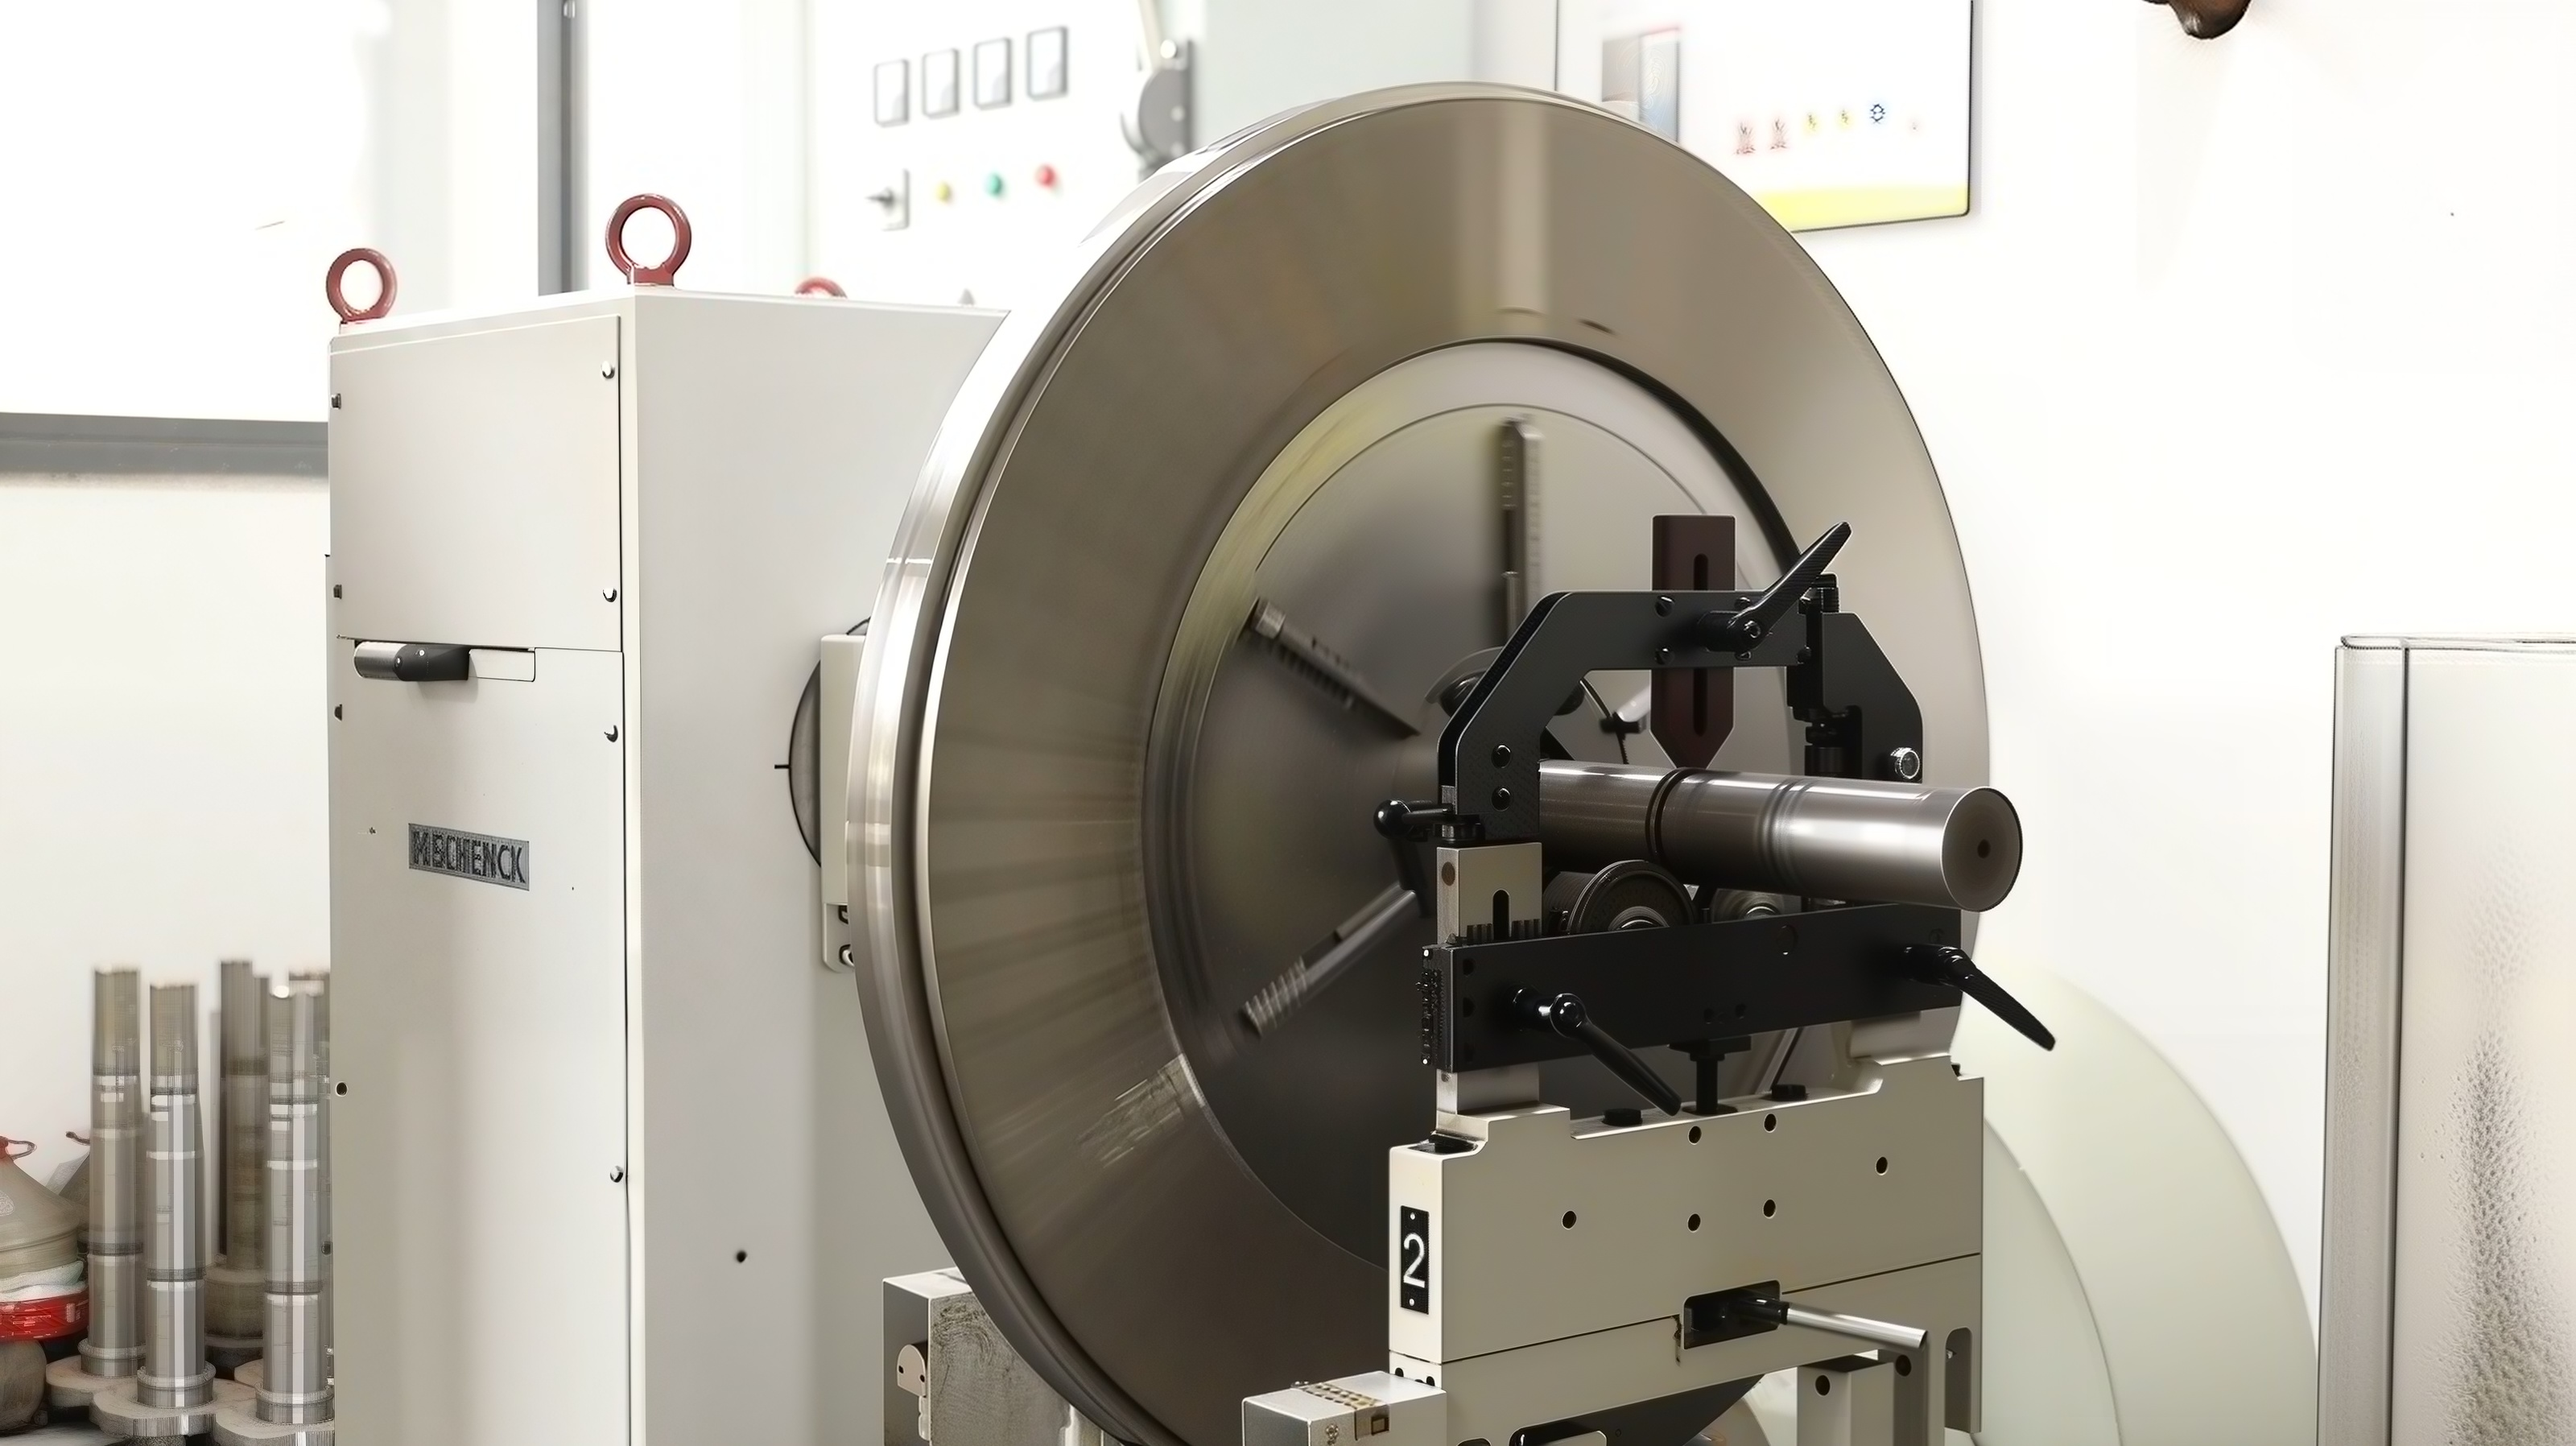
A high-speed plastic pulverizer requires more than a high-hardness cutting edge.
Dimensional consistency, blade geometry, correct installation, and rotor balance can also affect equipment operating stability.
Mao Yue's blade manufacturing process includes heat treatment, hardness testing, dimensional inspection, cutting-edge inspection, and dynamic balancing, which are incorporated into the production and quality control process.
There is no single material that is suitable for all operating conditions. D2 and DC53 can both be used for wear-resistant blades, but the specific choice should consider the plastic type, filler content, operating load, blade design, and heat treatment condition.
Not necessarily. Hardness is an important indicator of blade wear resistance, but actual service life is also affected by toughness, heat treatment, cutting-edge geometry, machining accuracy, processed material, and operating conditions.
Blade service life depends on the processed material, material throughput, target powder size, contaminants, cooling conditions, equipment configuration, and operating conditions. Therefore, operating time should always be considered together with the specific test conditions.
Blade wear can be evaluated through hardness testing, dimensional measurement, cutting-edge profile measurement, before-and-after blade photos, operating time, material throughput, and powder quality monitoring.
Both D2 and DC53 are tool steels that can be used in wear-resistant applications. Their suitability depends on the required hardness, toughness, wear resistance, heat treatment, and actual operating conditions.
Yes. Mineral fillers, glass fibers, and other hard components can increase abrasive loading and may accelerate blade wear compared with relatively clean polymers.
Customers can provide material information and, when conditions allow, actual material samples for testing and technical evaluation. Testing can consider the target powder size, throughput, temperature, feeding performance, and blade configuration.
A wear-resistant plastic pulverizer blade should not be defined by a single number.
Hardness matters. Steel grade matters. Heat treatment matters. But the most valuable evidence comes from actual production performance.
Can the blade maintain its working geometry?
Can the grinding gap remain stable?
Can the machine consistently produce powder within the target particle size range?
How much material can the blade process before replacement?
How does blade wear affect powder quality, output, and operating costs?
When these questions can be answered through controlled test data, wear resistance is no longer simply a marketing description. It becomes a measurable production performance indicator.
The right plastic pulverizer blade should be selected based on the actual processed material and production requirements, rather than simply according to a general specification sheet.
If you process PE, PP, PVC, color masterbatch, engineering plastics, filled plastics, or recycled plastics, you can provide Mao Yue with:
Material type
Feed size
Target powder particle size
Required throughput
Operating hours per day
Current blade problems
Final application
When conditions allow, you can also provide an actual material sample for testing.
Based on the material and production requirements, Mao Yue can further discuss suitable blade materials, hardness, pulverizing structure, cooling configuration, feeding system, and other equipment parameters.
The goal is not simply to supply a “wear-resistant blade,” but to develop a plastic pulverizing system that can consistently maintain the target powder quality while controlling blade replacement, maintenance, and operating costs.


