Specializing in the production of Plastic Pulverizer Machines.

Views: 0 Author: Site Editor Publish Time: 2026-10-16 Origin: Site
Even when a pulverizer appears to be operating normally, color masterbatch powder may still show inconsistent particle sizes. Some particles may be too coarse, others too fine, or the particle size distribution may change during continuous production.
These variations can affect powder handling, downstream processing, and production stability. Common causes include raw material variations, grinding disc wear, disc gap settings, temperature changes, unstable feeding, and screening issues. To choose an effective improvement measure, the first step is to identify where the particle size variation occurs.
The polymer carrier, pigments, fillers, and additives in color masterbatch can affect material hardness, toughness, thermal properties, and grinding behavior. Therefore, even when the pulverizer operating parameters remain unchanged, differences in formulation, material batch, or feed size may lead to variations in powder particle size distribution.
How to Check and Verify
Compare raw material information, formulation records, and feed sizes across different batches.
Where equipment conditions permit, test materials from different batches while keeping other operating conditions as consistent as possible.
Use the same sampling and particle size testing methods to compare the results from each batch.
If particle size changes coincide with changes in raw material batches and the differences remain under comparable equipment conditions, raw material properties may be one contributing factor. If both the raw materials and operating parameters change simultaneously, further testing is needed to distinguish their individual effects.
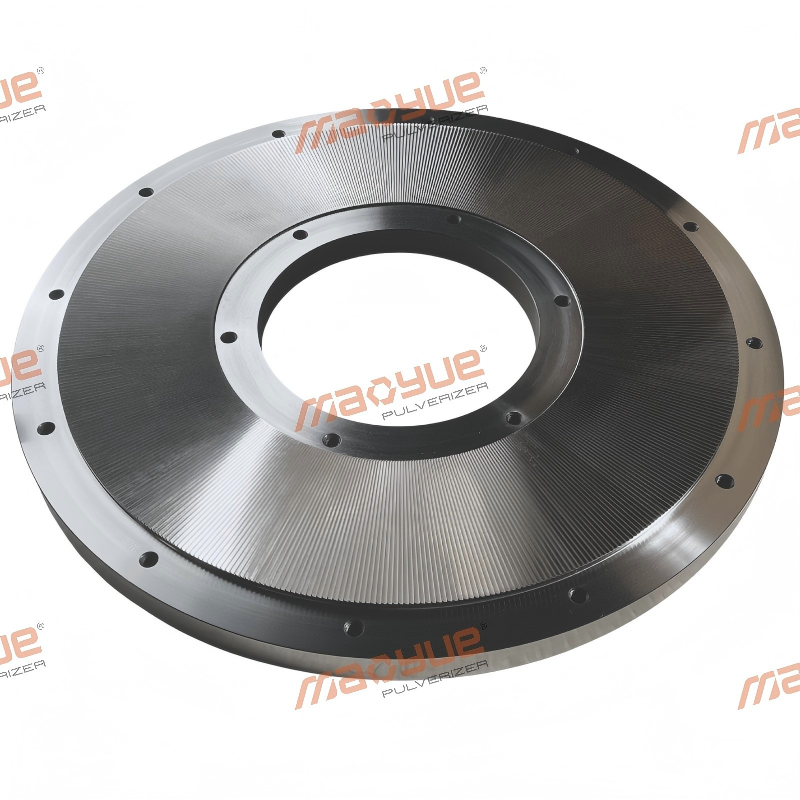
The geometry of the grinding disc working surface affects the grinding process. As the disc is used over time, it may develop wear, uneven damage, or material deposits, which can alter grinding performance.
Under otherwise similar conditions, these changes may increase the proportion of coarse particles or affect the particle size distribution. However, abnormal particle size results alone do not prove that the grinding disc is worn and should not be used as the sole basis for replacing it.
How to Check and Verify
Inspect the grinding disc working surface for uneven wear, damage, or material deposits.
Review component service records, maintenance records, and powder samples collected at different stages of operation.
Keep the raw material, feed rate, and grinding disc gap as consistent as possible when comparing particle size test results.
If visible abnormalities are found on the working surface and particle size changes persist under comparable operating conditions, grinding disc condition may be an important contributing factor. Comparing results before and after maintenance or component replacement can help verify this assessment, while accounting for any other changes in operating conditions.
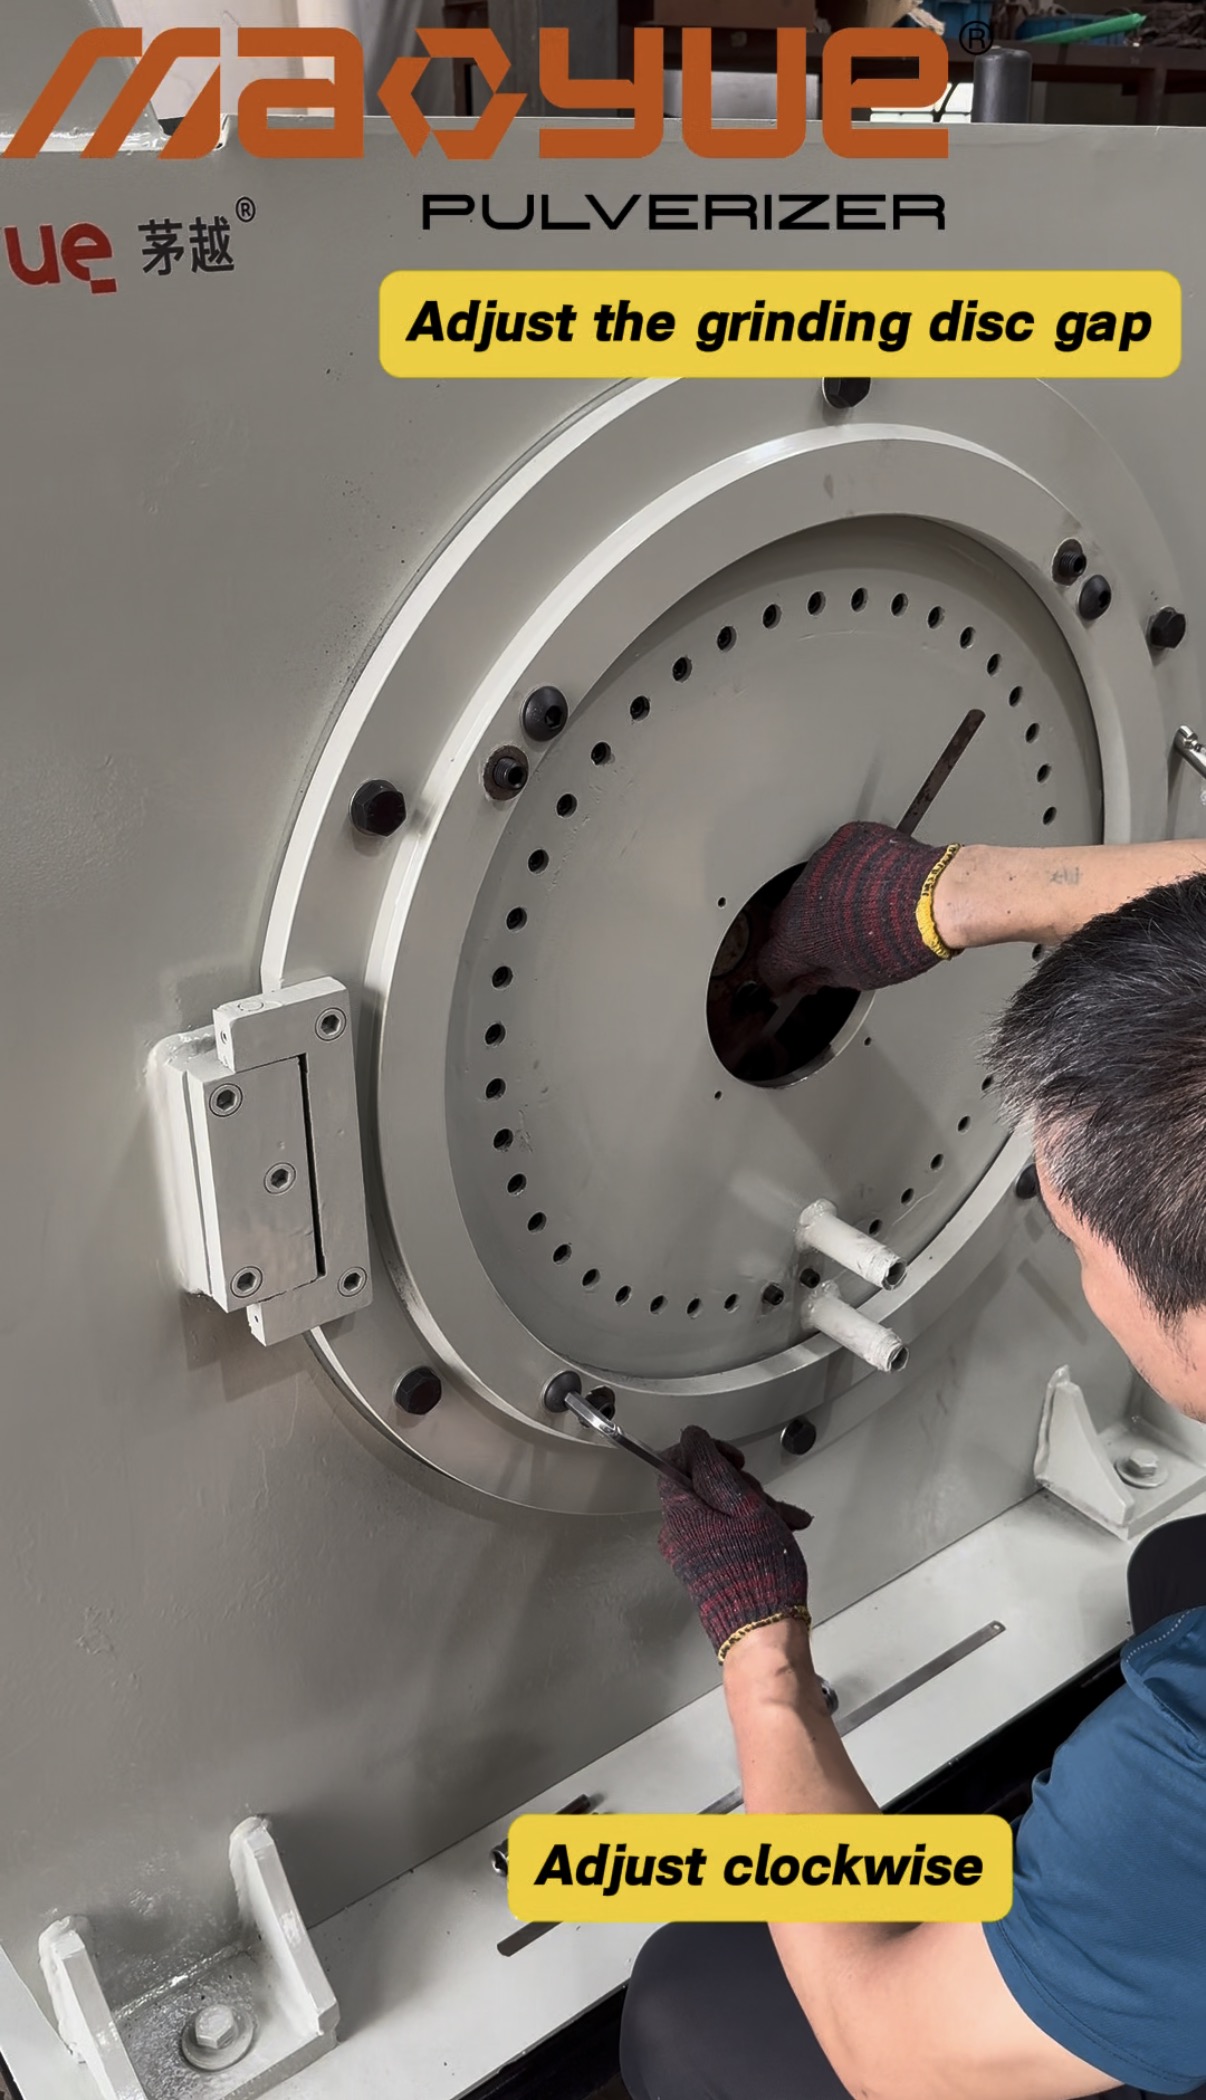
The grinding disc gap affects grinding intensity and the characteristics of the resulting powder. If the gap does not match the material properties and target particle size, the finished powder may contain too many coarse particles or an unsuitable proportion of fines.
A gap that is too wide may result in insufficient size reduction. Under certain equipment and material conditions, a gap that is too narrow may increase friction, heat generation, or mechanical load. Gap adjustment must therefore balance particle size requirements, throughput, and continuous operating stability rather than simply aiming for the smallest possible gap.
How to Check and Verify
Check whether the current gap setting matches the target powder specifications.
Verify that the adjustment mechanism can maintain the set gap consistently.
Within the equipment's permitted operating range, adjust one main variable at a time and compare the particle size distribution before and after the adjustment.
Record throughput and temperature at the same time to determine whether particle size improvements are accompanied by significant changes in other operating indicators.
If the adjusted setting brings the particle size distribution closer to the target range and produces similar results in repeat tests under comparable conditions, it may be better suited to the application. If there is little improvement, reassess other contributing factors instead of continuing to narrow the gap without sufficient evidence.
Mechanical grinding generates heat. Depending on the polymer carrier and formulation, rising temperatures may soften the material, increase its tendency to adhere to the grinding disc working surface, or cause fine particles to stick together and form agglomerates.
As a result, abnormally large particles in the finished powder are not necessarily caused by insufficient grinding. They may also be formed when smaller particles stick together. Distinguishing between these two conditions helps prevent inappropriate adjustments to the grinding parameters.
How to Check and Verify
Record temperature changes during startup and continuous operation.
Inspect the grinding chamber and working surfaces for material deposits or adhesion.
Compare powder samples collected during startup with those collected after the machine has been running for a period of time.
Use an appropriate testing method to assess whether the abnormal coarse particles may have formed through agglomeration.
If rising temperatures coincide with increased adhesion or agglomeration, thermal softening may be a contributing factor. If no obvious adhesion is observed but the proportion of coarse particles remains high, further checks of grinding conditions, component condition, and screening performance are necessary.

Stable feeding helps maintain a relatively consistent operating load inside the grinding chamber. If material enters the pulverizer intermittently, the equipment load may fluctuate, changing the conditions under which grinding takes place.
When particle size changes coincide with fluctuations in equipment load or feed rate, the feeding system should be inspected rather than immediately assuming that the grinding disc is worn or damaged.
How to Check and Verify
Observe whether material enters the pulverizer continuously and consistently.
Check the feeding system for bridging, material accumulation, or restricted discharge.
Compare feed rate, equipment load, and throughput records to determine whether particle size changes occur around the same time as feeding fluctuations.
After improving feeding stability, collect new samples using the same sampling method and compare the results.
If feeding fluctuations have a clear time relationship with particle size changes, and the powder becomes more consistent after feeding is stabilized, feeding conditions may be a contributing factor. If the problem persists after feeding becomes stable, investigate other stages of the process.

Grinding reduces material size, while screening separates particles according to the relevant separation conditions. Even if the powder leaving the pulverizer meets expectations, an unsuitable screening setup, damaged screen mesh, poor sealing, or material bypass can still affect the final product.
How to Check and Verify
Where the equipment layout permits, collect separate samples from the pulverizer outlet and the finished product after screening. Compare them using the same testing method.
If the pulverizer outlet sample already contains too many out-of-specification particles, investigate the raw materials and grinding conditions further.
If the outlet sample meets the requirements but the finished product does not, prioritize checks of screen integrity, screen specifications, sealing, and material bypass.
If particle size abnormalities may be related to material residue or contamination, also inspect downstream conveying, collection, and cleaning processes.
Comparing samples from different process stages helps identify where the particle size abnormality first appears and determine which areas should be investigated first.
If test results differ significantly before and after screening, further assessment of the screen specifications, screening efficiency, and material condition is necessary. The nominal screen opening alone cannot guarantee that the finished powder meets the target particle size range.
The first step in troubleshooting is to determine whether particle size differences occur between raw material batches or develop during continuous production of the same batch. It is also important to identify the earliest process stage at which the abnormality appears.
For differences between batches, prioritize comparisons of raw material information, formulation records, and feed size. For variations that develop over time within the same batch, evaluate grinding disc condition, material temperature, feed rate, and equipment operating records together.
If the problem may originate during screening or downstream handling, compare samples from the pulverizer outlet with those from the finished product whenever possible. This helps avoid attributing every particle size abnormality to the grinding process.
Once the potential contributing factors have been identified, control the main variables where possible and conduct comparisons using consistent sampling and testing methods. Evaluate the results against the target particle size specifications, selecting an appropriate method such as sieve analysis or laser diffraction according to the actual application. Results from different testing methods should not be directly compared without a valid basis for comparison.
After making an adjustment, compare the particle size distribution, proportion of out-of-specification particles, and relevant operating data. Results that can be reproduced under comparable conditions provide stronger evidence for identifying the cause and evaluating the adjustment. A single test can offer useful clues, but it may not be sufficient to confirm the root cause.
Observed Symptom | Priority Inspection Area | Recommended Next Step |
|---|---|---|
Particle size differs between material batches | Raw materials and feeding conditions | Compare batch records and test under comparable conditions |
Particle size changes during continuous operation | Grinding disc, temperature, and feeding system | Compare samples and equipment records from different operating periods |
Coarse particles increase alongside adhesion or agglomeration | Grinding surfaces and material temperature | Distinguish insufficient grinding from particle agglomeration |
The proportion of fines increases abnormally | Raw materials, grinding disc gap, and grinding conditions | Check target specifications and compare test results before and after adjustment |
Particle size changes coincide with temperature fluctuations | Cooling system and heat accumulation | Compare temperature trends with powder condition |
Pulverizer outlet powder meets specifications, but the finished product does not | Screening, conveying, and collection | Compare samples before and after each process stage to locate the abnormality |
Repeat tests produce significantly different results | Sampling, testing, and operating conditions | Standardize the testing method and repeat the comparison |
This diagnostic table helps prioritize inspections. It should not be used on its own to make a final determination of the root cause.
For color masterbatch powder, the goal is not simply to produce finer particles. The powder must meet the particle size requirements of the specific formulation, application, and downstream processing method.
A stable particle size distribution helps maintain consistent powder handling and feeding, reduce variations between production batches, and ensure that the finished powder remains closer to the required application specifications.
Particle size, however, is not the only factor that determines pigment dispersion or final product quality. Polymer carrier properties, pigment characteristics, formulation, and downstream processing conditions can also have an impact.
Therefore, grinding performance should be evaluated based on whether the powder consistently meets the target specifications and actual application requirements, rather than relying solely on average particle size or visual appearance.
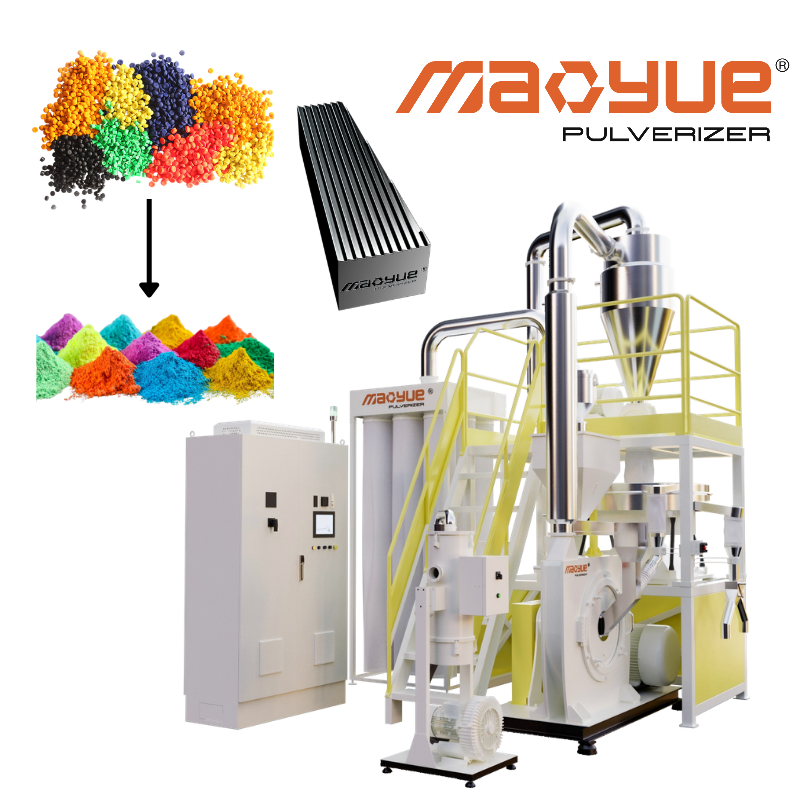
Inconsistent color masterbatch powder particle size does not necessarily mean that the entire pulverizer must be replaced. A more practical approach is to identify where the abnormality occurs first, then use test results to determine whether raw material preparation, grinding conditions, core components, or downstream screening should be addressed.
Mao Yue specializes in the R&D and manufacturing of disc-type plastic pulverizers. By combining actual material testing, in-house manufacturing of grinding discs and blades, and operating condition matching, Mao Yue can help customers evaluate grinding performance and equipment configurations based on their specific requirements.
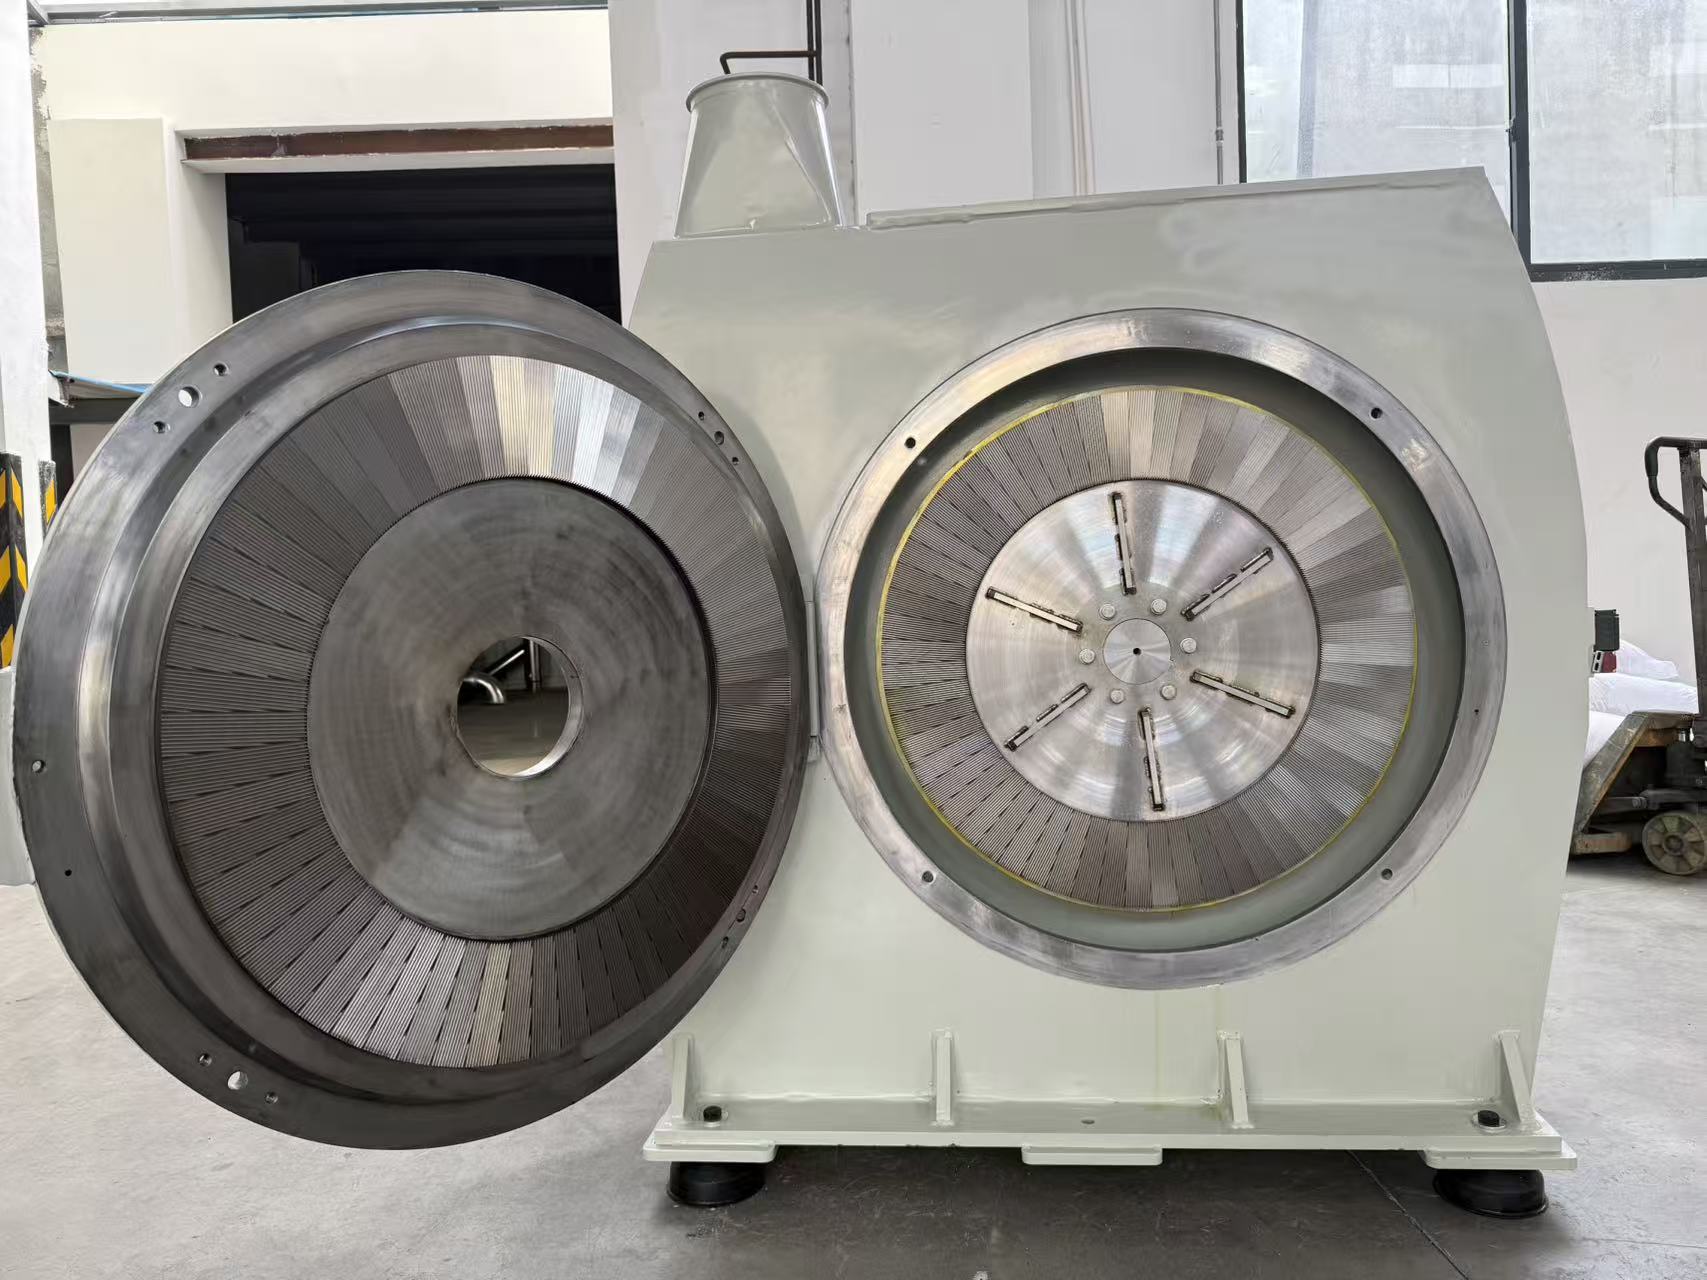
Different color masterbatch formulations can behave differently during grinding. The material name or target mesh size alone is not enough to determine how a pulverizer will perform under actual production conditions.
Where testing conditions permit, Mao Yue can test materials supplied by customers and record relevant results, including powder fineness, throughput, temperature changes, and operating conditions, according to the test scope.
Comparing these results with the customer's target specifications helps assess whether the current equipment configuration suits the application and whether further evaluation of grinding parameters or cooling conditions is needed.
For problems involving multiple contributing factors, additional testing may be necessary. A single test should not be treated as conclusive proof of the root cause.
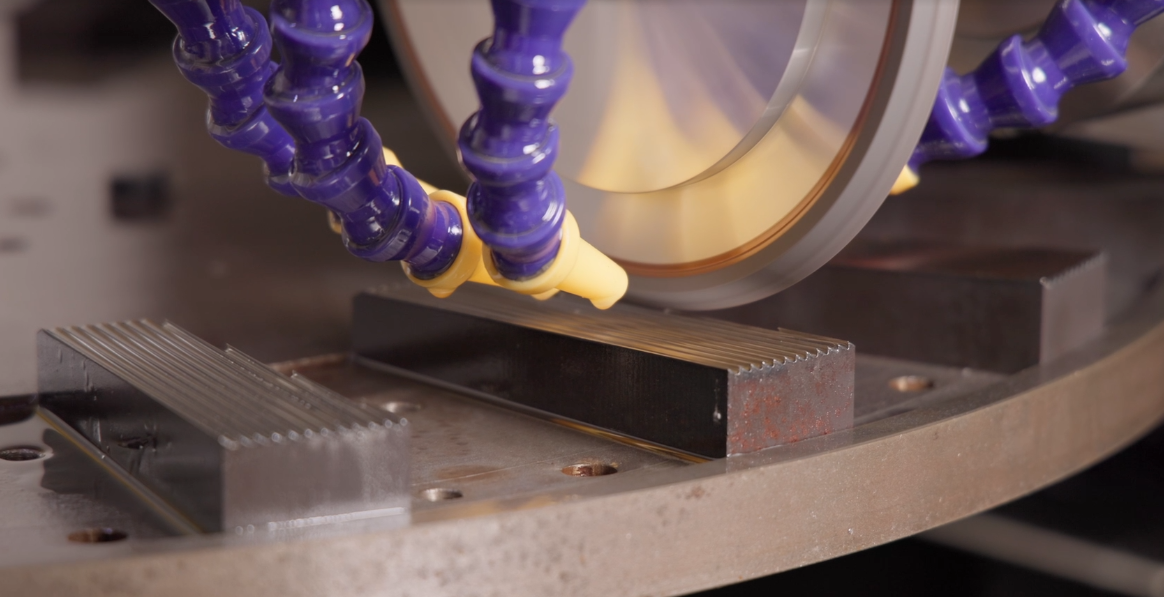
The condition of grinding discs and blades affects working geometry and grinding performance. Mao Yue manufactures its own grinding discs and blades, helping maintain control over the manufacturing and inspection processes for these core components.
When particle size changes over time, working surface inspections, component service records, and powder test results can be evaluated together to determine whether component condition may be affecting grinding performance.
If the available evidence does not justify component replacement, other operating factors should be investigated first. Comparing results before and after maintenance or replacement can provide a more reliable basis for future component management and help avoid replacing grinding discs solely because of a single abnormal particle size result.
Particle size consistency depends not only on grinding disc condition but also on the disc gap, feeding conditions, cooling configuration, and screening setup.
Mao Yue can evaluate relevant equipment configurations and operating conditions based on the customer's material properties, target particle size, and throughput requirements. Where conditions permit, comparing particle size distribution, throughput, and temperature before and after adjustments helps determine whether the changes have achieved the intended results.
If the abnormality actually originates in the screening or downstream processing system, the relevant system should be inspected first rather than continuing to adjust the grinding disc parameters.
This approach, based on actual material testing and operating data, helps customers select suitable equipment configurations and troubleshooting measures while reducing unnecessary parameter adjustments and component replacement.
If your color masterbatch pulverizer produces excessive coarse particles, an abnormal proportion of fines, powder agglomeration, or particle size variations between batches, you can provide Mao Yue with the following information for an initial assessment of your application requirements:
Material type: Polymer carrier and known formulation details.
Feed size: Original particle or material size.
Target particle size: Required mesh size or particle size range.
Target throughput: Expected processing capacity in kg/h.
Current problem: The observed issue and when or where it occurs in the production process.
If available, you can also provide particle size test results, temperature records, or samples collected at different stages of operation. This information can help narrow down the possible causes and determine whether actual material testing is needed.
Contact Mao Yue to discuss a plastic pulverizing solution tailored to your color masterbatch material, target particle size, and production requirements.


